Featured Automated Converting & Secondary Packaging Systems
Industrial-grade machinery engineered for uninterrupted high-speed production lines
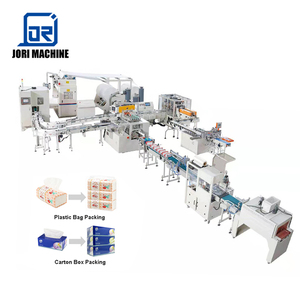
Industry Whitepaper: Modernizing End-of-Line Secondary Cartoning in Greater Boston's Paper Converting & Packaging Hubs
In the highly competitive manufacturing landscape of Greater Boston and the broader New England industrial region—encompassing key production zones along Route 128, I-495, and southern New Hampshire—operational efficiency is dictated by secondary packaging automation. As labor overhead costs across Massachusetts remain among the highest in the United States, paper converting plants, tissue mills, medical roll packagers, and FMCG contract manufacturers can no longer rely on manual carton erection, manual loading, and semi-automatic hot-melt taping. The transition toward fully automatic carton box packing machines (cartoners and end-of-line case packers) has evolved from a capital upgrade into a core operational necessity.
Andina Heavy Tissue Machinery S.A., drawing upon more than three decades of direct mechanical manufacturing experience since 1993, provides state-of-the-art automatic cartoning systems specifically configured to resolve the regional supply chain challenges faced by Boston-area plant directors. By merging robust multi-axis servo motion control with modular product feeding, high-speed rotary carton vacuum opening, and precise hot-melt glue or mechanical flap sealing, our machinery delivers the throughput, reliability, and low total cost of ownership (TCO) demanded by tier-one US paper converters.
Information Gain Key Takeaway: Transitioning from semi-automated secondary packaging to Andina's servo-driven continuous cartoning lines reduces per-carton packaging costs by up to 38% in Massachusetts facilities while ensuring 99.2% line availability at speeds exceeding 150 cartons per minute.
Mechanical Engineering Architecture of High-Speed Automatic Cartoning Systems
An automatic carton box packing machine functions as the central nerve hub of secondary packaging. It receives individual or bundled primary products—such as soft-pack facial tissue, interfolded paper towels, dinner napkins, medical hygiene rolls, or folded boxed goods—and automatically erects corrugated chipboard blanks, inserts the correct stack arrangement, and seals the carton flaps via tuck-in or hot-melt adhesive applications.
Our heavy-duty automatic cartoners are built on unified structural steel frames designed to suppress high-frequency mechanical vibrations during continuous high-speed execution. Below are the structural highlights that distinguish our equipment in the OEM marketplace:
Servo Synchronized Feeding
Independent multi-axis servo motors (Siemens / Schneider platforms) control infeed metering screws, product pushers, and carton transport chains with microsecond sync accuracy, eliminating product jams.
Rotary Vacuum Carton Extraction
Multiple rotary suction arms fitted with high-flow Venturi vacuum generators positively extract flat carton blanks from magazines, pre-breaking the score lines for perfect square box geometry every cycle.
Smart Vision & Reject Systems
Integrated photo-electric and vision sensors verify leaflet insertion, stack volume, and carton flap closure. Defective or incomplete cartons are automatically ejected via pneumatics without interrupting line flow.
To ensure total harmony between upstream paper converting units and downstream cartoning machinery, our lines utilize open-architecture PLC protocols with intuitive 10.4-inch color HMI touchscreens. Operators can store up to 200 distinct product recipes, reducing physical batch changeover times from hours to under 15 minutes.
Targeted Application Scenarios across Greater Boston & New England Manufacturing
The economic dynamics of Northeastern US manufacturing demand adaptable machinery that fits constrained facility footprints while complying with stringent regional energy and safety standards. Andina's automatic carton box packing machines are deployed across several specialized local industrial sectors:
1. Commercial & Away-From-Home (AFH) Tissue Converting
Facilities located in Worcester, Fitchburg, and the Merrimack Valley packaging bulk-use folded napkins, C-fold/multifold hand towels, and industrial wipes require high-capacity cartoning. Our machines handle heavy kraft paperboard boxes and multi-layer corrugated cases seamlessly, providing automated side-loading for high-density stacks.
2. Premium FMCG & Retail Boxed Tissue Packaging
Private-label retail tissue suppliers serving Boston metro consumer networks require flawless aesthetic presentation. Our cartoners utilize precise hot-melt glue application systems (compatible with Nordson units) to deliver clean, crisp carton seal lines without fiber tear or unsightly glue bleed-through.
3. Medical-Grade & Cleanroom Wipes Packaging
Boston's world-leading biotechnology corridor (Waltham, Cambridge, Lexington) demands zero-dust, stainless-steel-clad cartoning units for cleanroom-packaged sterile wipes and diagnostic tissue rolls. We provide optional 304/316 stainless steel frame constructions with HEPA laminar flow dust hoods.
4. E-Commerce & On-Demand Order Bundling Hubs
With major distribution facilities expanding along the I-95/I-495 beltway, our flexible cartoning lines enable rapid multi-pack assortment loading, allowing fulfillment centers to automatically pack mixed facial tissue boxes, wet wipes, and personal care paper goods into custom shipping containers.
Regional Industry Trends Impacting New England Packaging Buyers
Purchasing decisions in the Massachusetts packaging market are increasingly governed by evolving state environmental policies, labor demographics, and facility real estate costs. Understanding these localized vectors ensures that equipment investments yield long-term competitive advantages:
1. Mitigation of High Regional Electricity & Labor Overhead
Industrial power tariffs and hourly labor costs in New England rank among the highest in North America. Our cartoning systems feature regenerative servo braking technology and energy-efficient vacuum generation, reducing overall kilowatt-hour consumption by up to 22% compared to legacy pneumatic-heavy cartoners.
2. Transition to Recycled Corrugated Board & Lightweight Folding Cartons
Under Massachusetts Department of Environmental Protection (MassDEP) waste reduction goals, regional converters are shifting toward 100% recycled chipboard and thinner-gauge corrugated stocks. Traditional cartoners frequently struggle with variable board rigidity. Andina's adaptive vacuum pickers and motorized side-guide pressure tracks ensure reliable erection even when handling lightweight or non-virgin paperboard grades.
3. Footprint Optimization for Legacy Mill Infrastructure
Many New England paper converting plants operate within historic or retrofitted industrial facilities where floor space is premium. Our engineering team specializes in compact L-shape and U-shape cartoning layouts, maximizing throughput while staying within strict ceiling clearance and floor-load constraints.
Engineering Evaluation: Andina Automatic Cartoners vs. Legacy Western Systems
When evaluating international machinery suppliers against local European or North American equipment builders, Boston procurement managers weigh capital expenditure, build quality, and operational longevity. The table below outlines our comparative edge:
| Feature / Metric | Andina Heavy Tissue Machinery | Legacy North American OEM | Standard Entry-Level Cartoner |
|---|---|---|---|
| Drive Architecture | Full Servo Multi-Axis Sync (Siemens/Omron) | Hybrid Mechanical/Servo Drive | Chain Drive with Pneumatic Pushers |
| Max Cartoning Speed | 120 – 180 Cartons / Minute | 100 – 140 Cartons / Minute | 40 – 70 Cartons / Minute |
| Changeover Time | < 15 Minutes (Tool-Less Digital Indicators) | 30 – 45 Minutes | > 90 Minutes (Manual Adjustment) |
| Electrical & Safety Standard | UL-Compliant Components, CE Marked, NEMA 12 | UL / NFPA 79 Standard | Basic CE / Domestic Standard |
| Structural Framework | 15mm Annealed Steel Plate / CNC Machined | Cast Iron or Welded Steel Tube | Lightweight Aluminum Profile |
| Capital Investment ROI | Full Payback within 8 to 12 Months | Payback within 24 to 36 Months | Low Initial Cost, High Maintenance |
Corporate Strength & Manufacturing Authority: Andina Heavy Tissue Machinery S.A.
Established in 1993, Andina Heavy Tissue Machinery S.A. has spent over three decades establishing itself as a premier global manufacturer of tissue converting, paper folding, and automated packaging lines. Serving buyers in more than 160 countries across six continents, our company operates three state-of-the-art manufacturing centers located in Shanghai, Foshan, and Chengdu, spanning over 10,000 square meters of precision workshop space.
Our operational authority rests upon three unyielding structural pillars:
In-House CNC Machining Precision
Unlike regional integrators who outsource mechanical component fabrication to third-party machine shops, Andina operates its own high-precision CNC machining centers. From drive gears and rotary vacuum blocks to precision pusher arms, every critical component is milled in-house, ensuring micro-level dimensional tolerances and complete batch traceability.
Rigorous Quality Assurance & Patent Portfolio
Holding ISO 9001:2015 certification, CE safety compliance, and holding more than 50 national invention and utility patents, our machinery represents the pinnacle of Chinese heavy machinery engineering. Every automatic carton box packing machine undergoes a minimum 72-hour continuous dry-run and full-load test with customer-supplied tissue and board samples prior to export authorization.
End-to-End Overseas Service Infrastructure
We provide full technical support tailored for North American clients, including remote IoT diagnostic modules pre-installed on every control panel, English-language HMI interfaces, complete schematics, and rapid spare-part dispatch via global air express networks to Boston Logan Airport.
Frequently Asked Questions for New England Procurement Managers
Accelerate Your Packaging Automation in Greater Boston
Connect directly with our engineering department to request a customized technical proposal, 3D CAD layout, or ROI assessment for your automatic carton box packing requirements.
Inquire Now